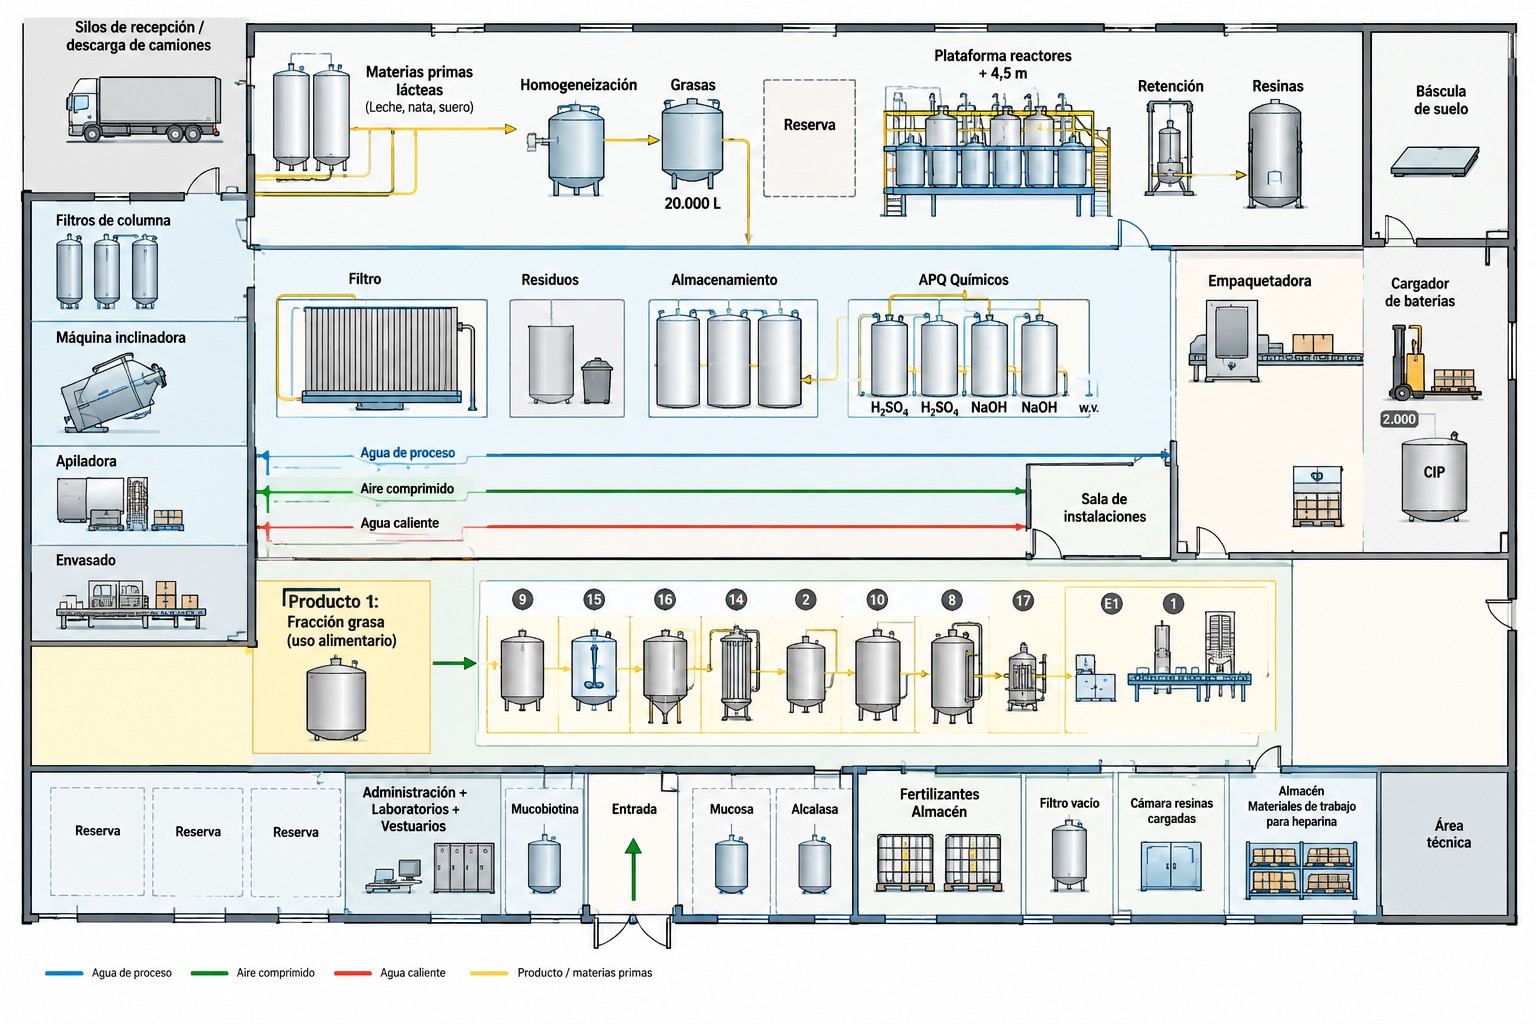
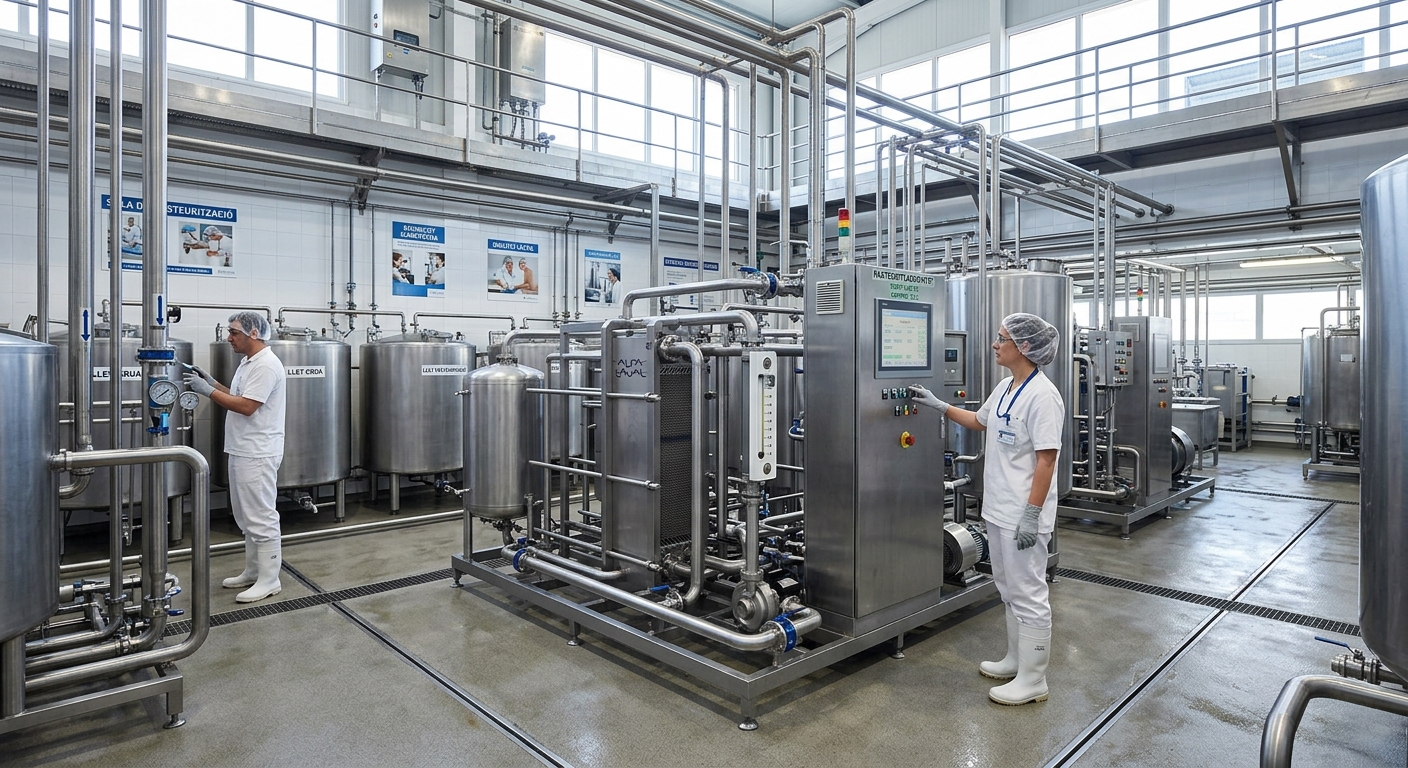
Plant layout for whey fractionation
The main technical challenge was integrating a membrane filtration system with varying pore sizes (microfiltration, ultrafiltration, and nanofiltration) coupled with highly energy-efficient evaporation and spray-drying equipment. A process architecture had to be designed to minimize protein denaturation, ensure absolute hygiene through automated cleaning (CIP) systems, and optimize water and energy consumption across all separation stages.
Our company’s work has focused entirely on the engineering, design, and initial project definition phase. This development has included drafting the technical report, preparing room layout drawings (for pasteurization, resin filters, steam boilers, and refrigerated areas), and defining process flow diagrams (P&IDs) and technical specifications for the subsequent selection of equipment and execution of the work.